


Send Message
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.


A mini refrigerated truck is a specialized commercial vehicle designed for the temperature-controlled transport of perishable goods in urban and regional logistics networks. Unlike standard cargo vans, these units integrate advanced thermal management systems to maintain precise internal temperatures, ensuring product integrity from origin to destination.
For procurement managers in the cold chain industry, selecting the right refrigeration unit is critical. Modern mini refrigerated trucks utilize high-efficiency heat pump technology and intelligent control systems to reduce energy consumption while maximizing payload capacity. This balance of cooling performance and operational efficiency makes them ideal for last-mile delivery, pharmacy distribution, and fresh food supply chains.
Dustproof and waterproof components ensure reliability in harsh operating environments, reducing downtime risks.
Advanced variable displacement technology significantly lowers daily energy consumption compared to standard units.
Cloud-based data systems allow real-time tracking of temperature and equipment status for proactive maintenance.
Zhengzhou Newbase Auto Electronics Co., Ltd. stands as a national "little giant" enterprise, recognized for its specialized R&D capabilities in thermal management systems. With three production bases spanning 40,000 square meters in Zhengzhou and Huangshan, NewBase delivers comprehensive solutions that meet rigorous international standards.
Our manufacturing process integrates fully self-developed underlying control technology, ensuring that every mini refrigerated truck component—from compressors to controllers—meets automotive-grade quality requirements. This vertical integration allows us to maintain strict quality control across the entire supply chain, from raw materials to final assembly.
Why this matters to you: Sourcing from a Tier 0.5 manufacturer like NewBase reduces your risk of supply chain disruptions while ensuring consistent quality across large fleet orders.
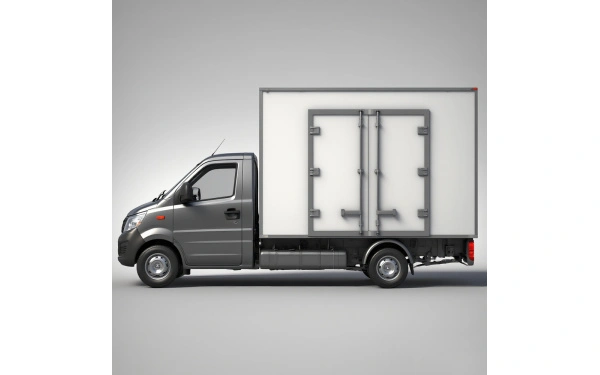
Selecting the optimal mini refrigerated truck requires evaluating several technical parameters beyond basic cooling capacity. The choice between standard heat pump systems and integrated battery thermal management solutions depends heavily on your specific operational environment and payload requirements.
Cooling Capacity & Efficiency: Look for units with full DC inverter technology, which can reduce weight by 30% while maintaining superior cooling performance. Units ranging from 18kW to 32kW cooling capacity are available for different vehicle sizes.
Integration Capabilities: Modern mini refrigerated trucks should offer integrated thermal management systems that combine air conditioning with battery cooling, reducing overall system cost by 30% and weight by 20%.
Intelligent Features: Prioritize vehicles with cloud platform connectivity for big data monitoring, allowing you to track temperature logs, predict maintenance needs, and optimize route efficiency.
Use this comprehensive checklist to evaluate potential suppliers and ensure your mini refrigerated truck investment meets all operational requirements.
Mini refrigerated trucks serve diverse industries requiring precise temperature control. Their compact size and advanced thermal management make them ideal for urban logistics where larger vehicles face restrictions.
Temperature-sensitive medications and vaccines require uninterrupted cold chain logistics. Mini refrigerated trucks with smart monitoring ensure regulatory compliance and product safety during last-mile delivery.
Perishable goods including dairy, meat, and produce benefit from consistent temperature control. Advanced heat pump technology maintains optimal conditions while minimizing energy costs for high-frequency urban routes.
Rapidly growing e-commerce sectors demand flexible cold chain solutions. Compact mini refrigerated trucks navigate narrow urban streets efficiently while providing reliable temperature control for consumer deliveries.
As a core Tier 1 supplier for major Chinese manufacturers including Yutong, Sinotruk, and CATL, NewBase brings unparalleled expertise in thermal management systems to the mini refrigerated truck market.
NewBase is the only domestic enterprise with fully self-developed underlying control technology for new energy thermal management systems. This vertical integration ensures quality consistency, faster innovation cycles, and competitive pricing for complete machine systems.
Since 2012, NewBase has maintained No. 1 market share in domestic commercial vehicle thermal management control systems. Our expertise extends to more than half of the bus industry market in new energy comfort electrical control systems.
With CAE/CFD simulation capabilities for 3-35kW systems and extensive testing facilities, NewBase develops innovative solutions including lightweight designs, high-efficiency heat pumps, and intelligent connectivity features that set industry standards.
With branches in Zhengzhou, Guangzhou, Shanghai, and other major cities, plus plans to export to over ten countries, NewBase provides comprehensive local support for international clients seeking reliable mini refrigerated truck partnerships.
Mini refrigerated trucks typically offer cooling capacities ranging from 18kW to 32kW, suitable for vehicles between 6-12 meters in length. Specific models include NBEAC-21 (18kW), NBEAC-24 (26kW), NBEAC-30 (30kW), and NBEAC-34 (32kW). These capacities can be customized based on your specific payload and ambient temperature requirements.
Integrated thermal management combines air conditioning and battery cooling systems into a single unit, reducing overall system cost by 30% and weight by 20%. This consolidation eliminates redundant components, simplifies installation, and improves energy efficiency through shared resources and intelligent control algorithms.
All critical components including compressors and electrical connectors achieve IP67 protection ratings, making them dustproof, waterproof, and vibration-resistant. These automotive-grade components can withstand submersion without damage, ensuring reliable operation in harsh weather conditions and wash-down scenarios.
Yes, our heat pump systems feature low-temperature air injection and enthalpy increase technology specifically designed for cold climates. In regions with temperatures as low as -10°C, these systems reduce average daily energy consumption by over 30% compared to standard heat pump air conditioning, ensuring efficient heating performance even in extreme cold.
Modern units include intelligent interaction systems supporting infrared, Bluetooth, WiFi, and voice control. Cloud platform big data systems enable remote monitoring via PC software or mobile apps, providing real-time temperature tracking, fault diagnosis, and predictive maintenance alerts to minimize downtime and optimize fleet operations.
NewBase maintains quality through complete industry chain control, from self-developed control technology to component manufacturing. Our 40,000 square meter production facilities in Zhengzhou and Huangshan employ rigorous testing protocols including CAE/CFD simulations, EMC testing meeting national standard level I, and comprehensive durability validation before shipment.
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
Fill in more information so that we can get in touch with you faster
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.