


Send Message
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.


A cold chain refrigeration container is a specialized logistics unit designed to maintain precise temperature control for perishable goods during transit. Unlike standard shipping containers, these units integrate advanced thermal management systems to ensure pharmaceuticals, fresh produce, and frozen foods remain within strict quality parameters from origin to destination.
Why It Matters: Investing in high-quality refrigeration infrastructure reduces spoilage risks and ensures compliance with international food safety standards, protecting your brand reputation and minimizing financial loss.
Modern solutions leverage autonomous driving capabilities and intelligent thermal control to optimize energy efficiency while providing real-time monitoring of cargo conditions.
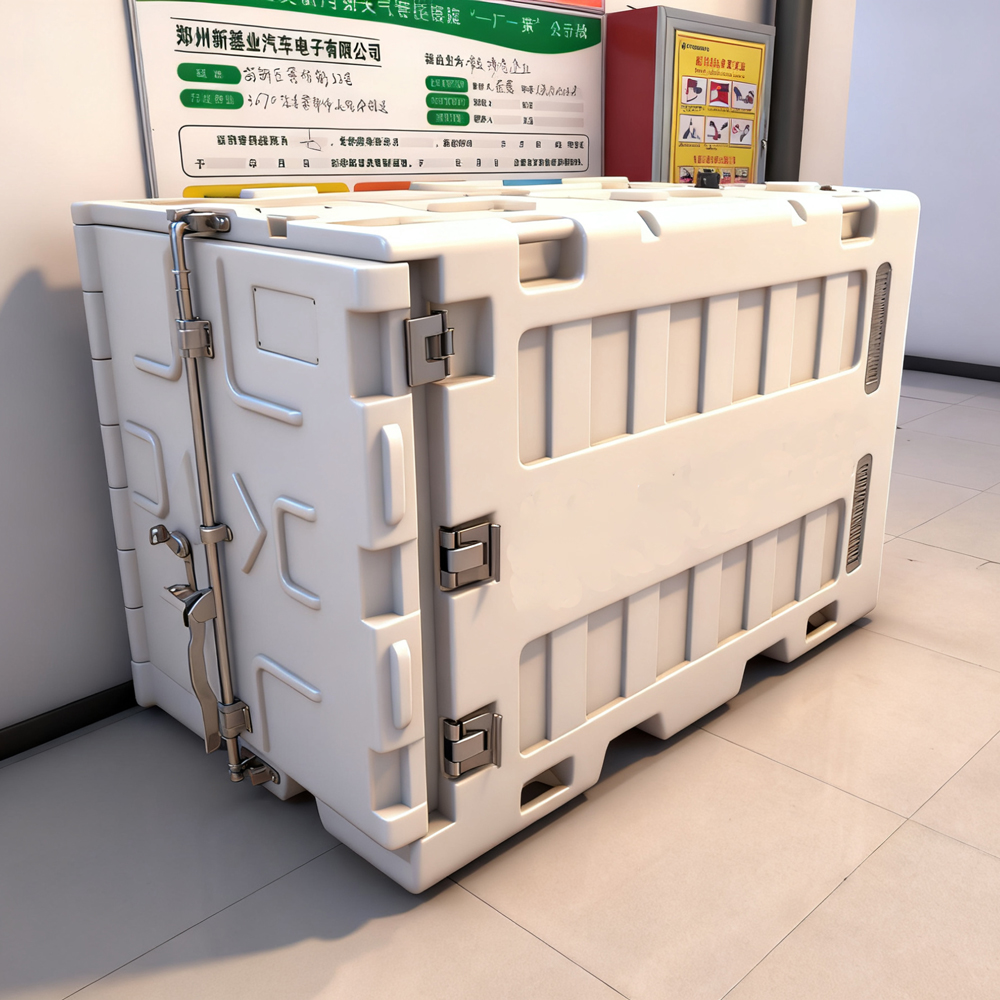
As a designated "little giant" enterprise by the Ministry of Industry and Information Technology, NewBase possesses comprehensive R&D capabilities for complex thermal management systems.
Our expertise in variable displacement control and low-temperature air injection technology allows us to reduce daily energy consumption by over 30% in extreme environments (-10°C).
NewBase is the only domestic enterprise with fully self-developed underlying control technology for new energy thermal management systems.
We cover the entire industry chain from R&D to manufacturing, offering Tier 0.5 complete machine support that simplifies procurement and ensures component compatibility.
Since 2012, we have maintained the No. 1 market share in domestic commercial vehicle thermal management control systems.
Trusted by major manufacturers including Yutong, Sinotruk, SAIC Maxus, and CATL, our technology powers thousands of vehicles globally.

Our three production bases in Zhengzhou, Jiaozuo, and Huangshan are equipped with advanced CAE/CFD simulation capabilities and rigorous testing protocols.
Component Protection: All critical components achieve IP67 protection ratings, ensuring dustproof and waterproof performance even when submerged, meeting automotive-grade durability requirements.
EMC Compliance: Our systems meet national Level I EMC standards, passing third-party testing to prevent electromagnetic radiation hazards and ensure reliable operation in complex electrical environments.
Look for suppliers who offer integrated battery and cabin thermal management. NewBase's compact integration reduces costs by 30% and weight by 20% compared to separate systems.
Multi-channel electronic expansion valves and smart PID control ensure precise cooling distribution between cargo and battery compartments.
Prioritize units featuring full DC inverter technology and PWM stepless speed regulation. These technologies enable flexible variable frequency operation, significantly lowering power consumption.
Variable displacement control coupled with electronic expansion valves optimizes refrigerant flow based on real-time temperature differentials.
Cloud platform connectivity allows for big data monitoring, analysis, and storage of equipment status via PC software or mobile apps.
Smart interaction systems supporting Bluetooth, WiFi, and voice control provide convenient operational access and remote diagnostics.
When evaluating cold chain refrigeration container suppliers, use this checklist to verify technical capability and reliability:
Core Strength: Full-chain ecosystem for new energy commercial thermal management products, from control systems to complete machines.
Key Advantage: Only domestic enterprise with fully self-developed underlying control technology and core components across the entire industry chain.
Market Coverage: Exclusive supplier for Yutong, Zhongtong, Sinotruk, SAIC Maxus, and other leading manufacturers.
Global Support: Branches in Zhengzhou, Guangzhou, Shanghai, Nanjing, Xi'an, and Jinan, with export plans to over ten countries including the US, Spain, India, and Turkey.
R&D Capability: 40,000 square meter production base with comprehensive CAE/CFD simulation and thermal system testing capabilities.
Innovation Focus: Continuous investment in lightweight technology, heat pump efficiency, and intelligent connectivity solutions.
Temperature-sensitive vaccines and biologics require precise climate control. NewBase's systems maintain stable temperatures with minimal fluctuation, ensuring drug efficacy throughout the supply chain.
Perishable goods benefit from optimized airflow design and humidity control systems. Our V-shaped shock absorption and noise reduction technology ensures gentle transport conditions.
Integration with autonomous logistics vehicles enables unattended cold chain operations. Cloud-based monitoring provides real-time visibility into cargo conditions without manual intervention.
Problem: Integrated units often struggle with uneven cooling between cabin and battery compartments.
Solution: NewBase pioneers multi-channel electronic expansion valves and P+T pressure sensors with smart PID control to precisely adjust compressor speed and refrigerant flow distribution.
Problem: Standard heat pumps lose efficiency in freezing conditions, increasing energy costs.
Solution: Low-temperature air injection and enthalpy increase technology reduces average daily energy consumption by over 30% in -10°C environments compared to conventional systems.
Problem: High-voltage systems in electric vehicles create electromagnetic noise affecting control electronics.
Solution: 360° shielding and equipotential connection protection effectively prevent interference, enhancing reliability of electronic components in complex EM environments.
Problem: Frequent component failures lead to costly downtime and repairs.
Solution: IP67-rated components and automotive-grade connectors ensure durability. Remote monitoring and diagnostic capabilities enable predictive maintenance before failures occur.
NewBase offers several distinct advantages: first, we are the only domestic enterprise with fully self-developed underlying control technology for new energy thermal management systems. Second, our full-chain integration reduces costs by 30% and weight by 20%. Third, our low-temperature air injection technology reduces energy consumption by over 30% in -10°C environments. Finally, our IP67-rated components ensure durability in harsh conditions.
We utilize computer-aided engineering (CAE/CFD) simulations to optimize airflow distribution and temperature fields within the container. Our unique in-vehicle temperature and humidity control system aligns with European comfort curves, supported by deep research through our postdoctoral program. Additionally, our dual-system, dual-return structure enables zoned temperature control for precise cargo management.
We source premium components from industry leaders: Highly or Copeland compressors, Fenstars/EBM evaporator fans, Fenstars/SPAL condenser fans, and Danfoss/Sanhua electronic expansion valves. All controllers, DC-DC modules, and high/low voltage electrical boxes are manufactured in-house by NewBase, ensuring perfect integration and quality control.
Yes. As a Tier 0.5 supplier, we offer complete machine R&D and manufacturing tailored to specific requirements. Our modular design allows customization of cooling capacity (3-35kW range), structural forms, and integration levels. We work closely with clients to develop solutions for pure electric, hybrid, and fuel cell vehicles.
NewBase has branches in Zhengzhou, Guangzhou, Shanghai, Nanjing, Xi'an, and Jinan. We plan to export complete air conditioning systems to more than ten countries including Iran, the United States, Spain, India, and Turkey. Our technology currently powers vehicles for major manufacturers across China and is expanding internationally.
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
Fill in more information so that we can get in touch with you faster
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.