


Send Message
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.


An IoT-enabled mobile cold chain box is a high-tech refrigerated transport solution that integrates advanced thermal management with real-time digital monitoring. Unlike traditional cold storage units that operate blindly, these systems provide continuous visibility into temperature, humidity, and equipment health throughout the journey.
Powered by NewBase's expertise in new energy thermal control, this technology ensures that sensitive goods—from pharmaceuticals to fresh produce—remain within strict environmental parameters. By combining robust hardware with intelligent software, it eliminates data gaps and reduces the risk of spoilage or regulatory non-compliance.
As a designated "little giant" enterprise by China's Ministry of Industry and Information Technology, NewBase brings over 15 years of specialized R&D to mobile cold chain. We hold No. 1 market share in domestic commercial vehicle thermal management control systems, ensuring you partner with the industry benchmark.
We don't just assemble parts; we manufacture core components across the entire industry chain. From self-developed underlying control technology to the final assembly of micro new energy cold chain vehicles, our vertical integration guarantees superior quality and consistent performance for your supply chain.
Our IoT systems utilize variable displacement and low-temperature air injection technologies to reduce daily energy consumption by over 30%. This efficiency lowers your total cost of ownership while extending the operational range of electric fleet vehicles.
With branches across major Chinese cities and export plans spanning Europe, Asia, and the Americas, NewBase provides a global support network. Our IP67-rated components ensure durability in harsh environments, protecting your cargo regardless of the route conditions.
NewBase’s manufacturing capability is backed by three large-scale R&D and production bases covering 40,000 square meters. We utilize advanced CAE/CFD computer simulations to optimize every component before it reaches the factory floor.
Key Quality Standards:

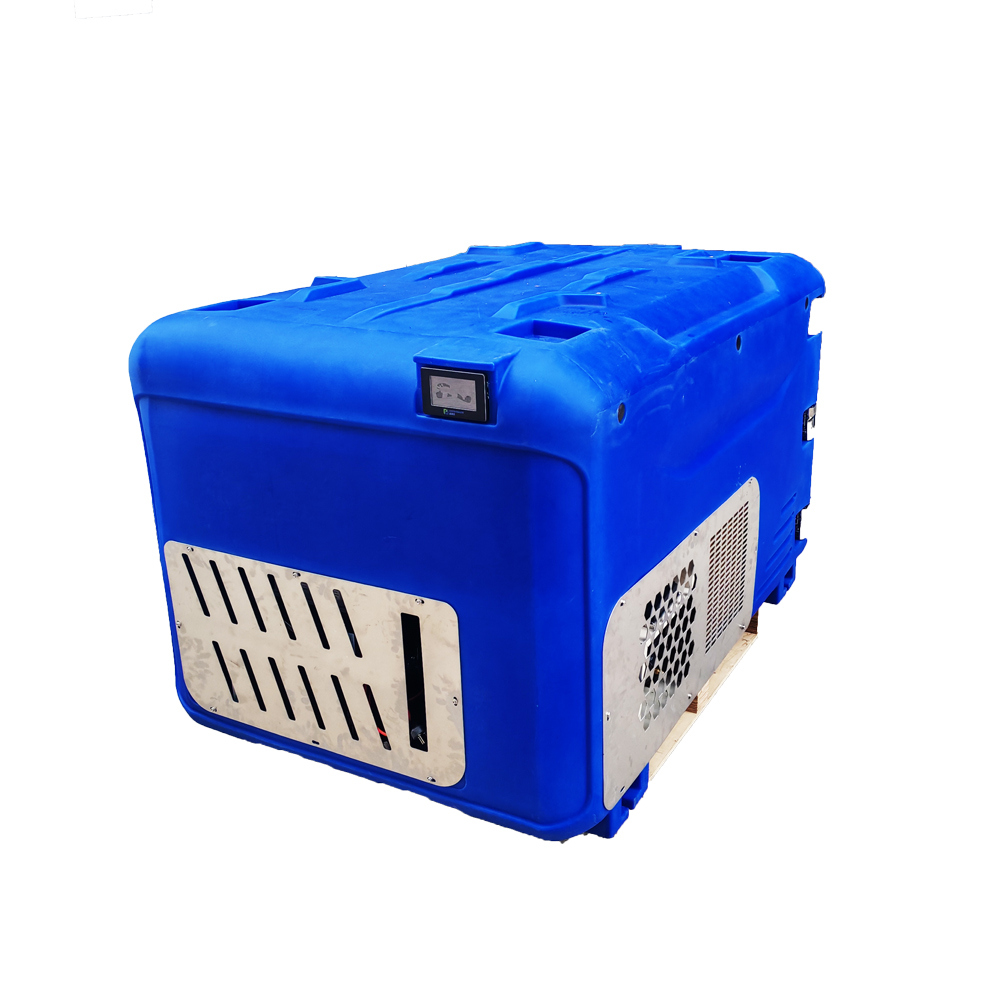
Selecting the correct mobile cold chain box requires balancing payload capacity, thermal stability, and connectivity features. Here is what procurement buyers should prioritize:
Ensure the manufacturer uses top-tier compressors (like Highly or Copeland) and precise sensors (Danfoss/Sanhua). NewBase integrates these premium brands to guarantee long-term reliability.
Look for solutions that integrate battery thermal management with cabin cooling. This dual-function approach can reduce system weight by 20% and costs by 30% compared to separate units.
The best IoT boxes offer cloud platform access via PC or mobile app. You need immediate alerts for temperature deviations to take corrective action before cargo is compromised.
Does the unit maintain temperature within ±0.5°C variance during door openings and extreme weather?
Is the cooling system designed with PWM fan control and variable frequency drives to minimize battery drain?
Does the IoT module support Bluetooth, WiFi, and cellular data for seamless tracking in remote areas?
Are all electrical components rated IP67 or higher to withstand high-pressure washing and vibration?
Does the supplier offer comprehensive after-sales service and rapid spare part delivery globally?
Can the system be tailored to specific payload sizes and voltage requirements for your existing fleet?
Move beyond standard Tier 1 suppliers. Partner with manufacturers like NewBase who have evolved into Tier 0.5, offering complete machine R&D and manufacturing. This level of partnership allows for deeper customization and faster innovation cycles.
Choose a supplier with a strong postdoctoral research station and extensive patent portfolio. Their ability to simulate and test thermal systems internally means fewer bugs and higher efficiency in the final product delivered to you.
Strict temperature adherence for vaccines and biologics, supported by unbroken digital audit trails required by regulatory bodies.
Rapid cooling and stable humidity levels extend the shelf life of perishable goods, reducing waste and maximizing profit margins.
Robust, explosion-proof designs with smart monitoring ensure safe transport of temperature-sensitive industrial chemicals.
With proper maintenance, NewBase cold chain units are engineered for a lifespan of 10-15 years. The use of durable materials like SMC/LFT-D and high-grade compressors ensures long-term structural integrity.
The onboard controller stores data locally when connectivity is lost and automatically syncs to the cloud platform once a signal is restored, ensuring no data gaps in your shipment records.
Yes, NewBase offers open API interfaces that allow for seamless integration with most third-party logistics and fleet management platforms.
We provide comprehensive warranties on all core components, including compressors and controllers, backed by our global network of service centers for quick repairs.
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.
Fill in more information so that we can get in touch with you faster
Privacy statement: Your privacy is very important to Us. Our company promises not to disclose your personal information to any external company with out your explicit permission.